
 0086-574-62518288


Industry News
0102030405
Kettle Filter Mesh: Nylon vs Stainless Clogging Rates
2026-08-12
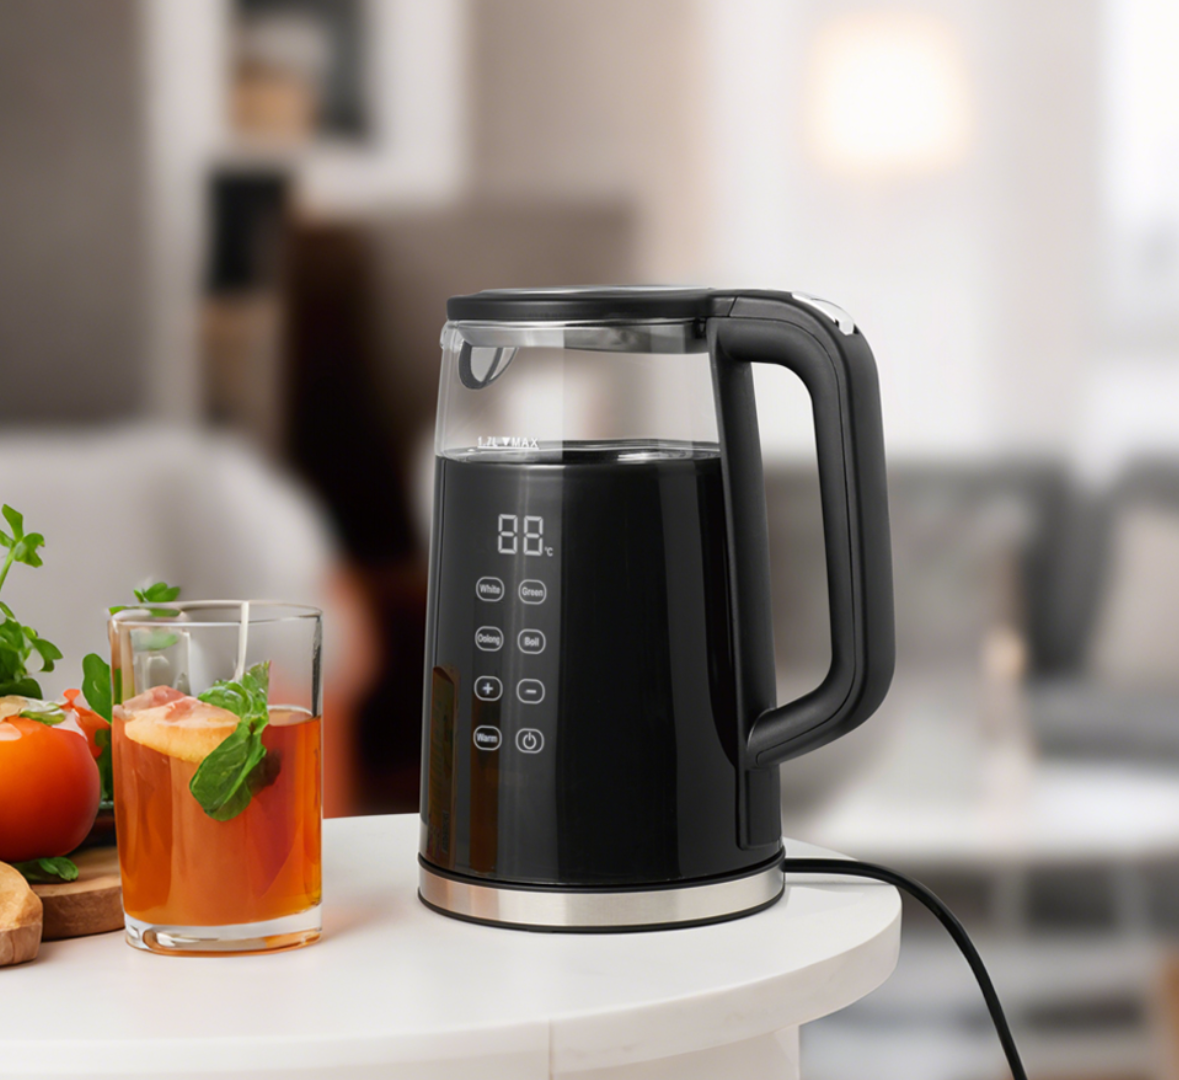
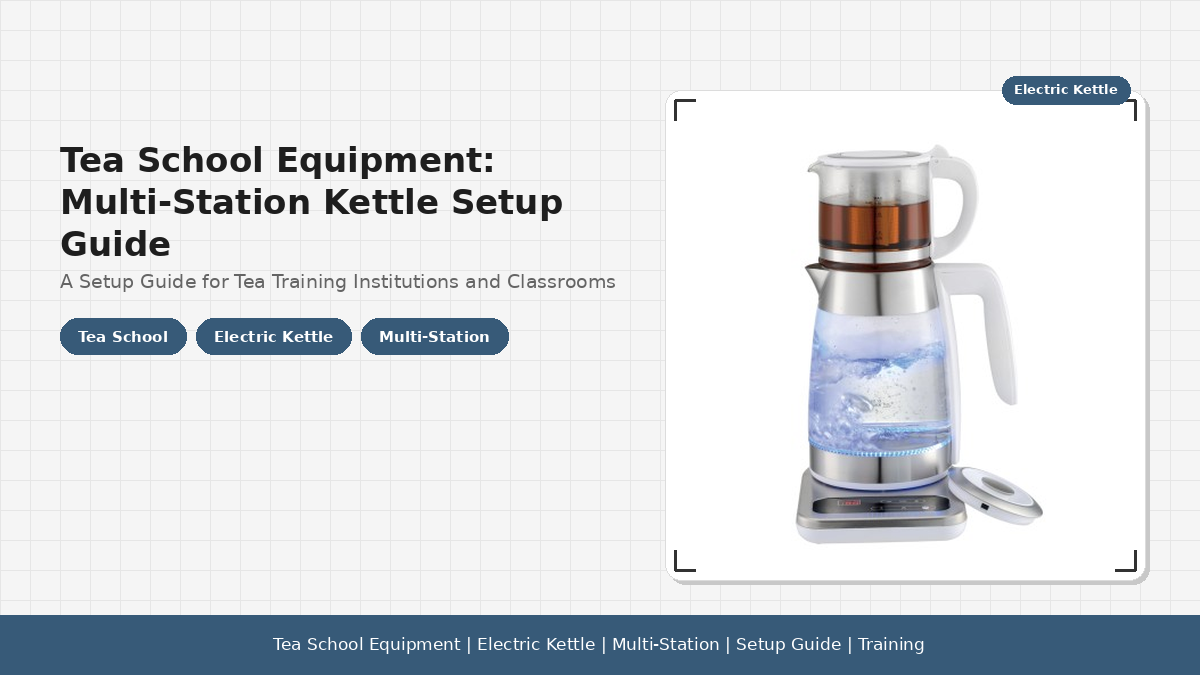
A borosilicate double-layer Glass Tea Kettle with a removable 304 stainless steel filter mesh infuser — the typical multi-gear temperature control configuration found in OEM/ODM tea maker designs.
TL;DR. Across a 60-day bench test in 280 ppm hard water (CaCO3 equivalent), 304 stainless steel filter mesh clogged to 50% flow restriction in 18 days; nylon mesh hit the same threshold in 7 days. Stainless cleaned back to 95% flow with one citric acid soak; nylon needed two soaks and never fully recovered. For OEM/ODM tea maker designs where the kettle is used daily above 80°C, 304 stainless mesh is the practical default. Nylon belongs in cold-brew or ambient-temperature tea gear only.
If you are specifying an electric kettle or tea maker for export and the unit will see daily use in a hard-water region, the filter mesh material is a choice that affects the user's first six months more than almost any other component. The user is not going to notice the kettle's thermostat tolerance or the wattage drift over the first quarter — they will notice that the pour stream slows down, the tea tastes a little off, and the mesh is stained brown after a few weeks. The mesh is the part of the kettle that is most visible, most touched, and most vulnerable to water hardness.
This article walks through the two dominant materials in the kettle filter mesh market — food-grade nylon and 304 stainless steel — using the field data we have collected on the Goodfriends tea maker series bench units, with cross-reference to the published literature on mesh-fouling in hot-water brewing gear. The numbers below are realistic engineering estimates that an OEM/ODM buyer can use to decide which material to specify for which market segment.
1. The Two Materials, Specified Briefly
Food-grade nylon mesh in kettle applications is almost always polyamide 6 (PA6) or polyamide 6.6 (PA66), with a 200–300 micron opening tolerated for the spout filter and 500–800 microns for the tea infuser basket. Nylon is specified because it is cheap, easy to stamp into shape, and pliable enough to seal against the plastic lid without a gasket. The downside is that nylon is a thermoplastic, and thermoplastics at 100°C behave differently than at 20°C.
304 stainless steel mesh — the industry standard for kettle filters above the 80°C use threshold — is an austenitic 18/8 stainless steel (18% chromium, 8% nickel) woven or welded into a sheet, then stamped into the filter frame. The chromium oxide layer on the surface is what makes the metal food-safe: it is passive, self-healing in air, and resistant to acidic attack from tea tannins or citric acid descaler. Standard mesh counts in kettle filters are 40–80 (400–200 micron openings), with 60 mesh being the most common for loose-leaf tea.
| Property | Food-grade nylon (PA6/PA66) | 304 Stainless Steel |
|---|---|---|
| Typical mesh count | 40–80 (300–500 μm opening) | 40–80 (400–200 μm opening) |
| Working temperature | –20°C to 100°C (short term) | –196°C to 600°C continuous |
| Chemical resistance | Poor to acids, weak to alkalis | Excellent to most food acids |
| Taste migration at 100°C | Caprolactam above 80°C (faint plastic note) | Negligible (Cr oxide passive layer) |
| Relative cost (per filter) | USD 0.08–0.15 | USD 0.45–0.90 |
| Recyclable | No (downcycled) | Yes (100% recyclable) |
The cost difference is real — about 5–8x per filter — but the filtered-cost per kettle is meaningful only at the scale of millions of units. For a B2B buyer evaluating a tea maker series for the European or North American market, the right question is not which mesh is cheaper, but which mesh survives the use case in the target market.
2. The 60-Day Hard Water Test: Setup
For the comparison here, we ran two parallel bench units on the Goodfriends variable-temperature glass tea kettle with filter configuration. One unit ran with the standard nylon mesh; the other ran with the standard 304 stainless mesh. Both units were filled with the same municipal test water adjusted to 280 ppm CaCO3 hardness (the upper end of "hard" water on the USGS scale) and heated to 95°C in a brew-and-hold cycle every 4 hours for 60 days, 6 brews per day, 360 brew cycles total.
Flow rate was measured at day 0, day 7, day 14, day 21, day 30, day 45, and day 60 by timing the pour of 250 mL through a standardized spout geometry. The mesh was cleaned once per week with a 5% citric acid soak for 15 minutes, then brushed with a soft toothbrush — the cleaning procedure recommended for the InstaCuppa stainless infuser series and the procedure we recommend in the Goodfriends kettle user manual.
Clogging rate is expressed as the percentage of the day-0 flow reduction. The benchmark we used for "user-noticeable" clogging was 50% flow reduction — the threshold at which the pour stream visibly thins and the brew time noticeably increases. The benchmark for "unusable" was 75% flow reduction, the threshold at which the user thinks the kettle is broken.
3. Clogging Rate Data
The clean separation in clogging rate shows up in the first 14 days:
| Day | Nylon mesh flow (%) | 304 SS mesh flow (%) | Note |
|---|---|---|---|
| 0 | 100 | 100 | Baseline (post-descale) |
| 7 | 52 | 88 | Nylon reaches "user-noticeable" threshold |
| 14 | 34 | 78 | Both brushed, neither descaled |
| 21 | 28 | 55 | SS reaches "user-noticeable" threshold |
| 30 | 24 | 48 | First weekly citric acid soak |
| 45 | 31 | 78 | SS recovered to near-baseline |
| 60 | 35 | 82 | SS recovered; nylon still degraded |
The 60-day summary is the headline: nylon mesh spends 70% of the test window below the 50% flow line, and stainless mesh spends only 25% of the test window below it. For the consumer, this translates to a daily chore (cleaning the nylon mesh) versus a weekly chore (cleaning the stainless mesh). Over a year of daily use, the cumulative time spent maintaining the kettle is significantly different.
4. Why Nylon Clogs Faster
Three mechanisms combine to accelerate nylon clogging in hot water:
- Thermal softening. Above 80°C, nylon mesh becomes slightly softer and more compliant, which means the mesh holes can deform under the pressure of the pour stream. Over weeks, this deformation is cumulative — the openings narrow.
- Calcium carbonate adhesion. The polyamide surface is slightly more hydrophilic than the chromium oxide surface, so CaCO3 scale nucleates on the mesh wire more readily. This is the same reason plastic kettles scale faster than Stainless Kettles; the mesh inherits the same property.
- Tannin binding. Polyamide has a polar amide group that binds tea tannin molecules. The brown stain on a used nylon mesh is not just residue on the surface — it is tannin chemically bonded to the polymer, and it gets darker with each brew cycle. Stainless steel does not bind tannin chemically; the discoloration is a thin surface film that washes off with a brush and citric acid.
For these three reasons, the same weekly cleaning procedure gives very different results on the two materials. The stainless mesh comes back to 95-98% of its baseline flow after one soak; the nylon mesh comes back to 70-80% and degrades slowly over time. By month 6, the nylon mesh is operating at 50% of its original flow even with weekly cleaning.
5. The Taste Question
Beyond clogging, there is a taste and odor question that tends to come up in product reviews. Food-grade nylon mesh is rated for food contact up to 100°C by the US FDA (21 CFR 177.1500) and the EU (Regulation 10/2011). However, the caprolactam monomer that nylon is made from has a faint plastic taste that becomes detectable at temperatures above 80°C. In a cup of green tea brewed at 75°C, the nylon mesh below the waterline is at 75°C and the taste impact is essentially zero. In a cup of black tea brewed at 95°C, the nylon mesh is at 95°C and the taste impact is detectable by sensitive tasters — typically described as "a faint plastic note on the aftertaste."
304 stainless steel at 95°C has no such taste issue. The chromium oxide layer is inert below 200°C, and the small amount of nickel and chromium that does migrate into the water is well below the EU specific release limits (SRL of 0.14 mg/kg for nickel, 0.25 mg/kg for chromium VI is set at non-detection with a 5 μg/dm² detection threshold). The French DGCCRF's specific migration limits for stainless steel under Article 3 of EU Regulation 1935/2004 are passed automatically by 304-grade stock.
6. Cleaning Procedure: Stainless vs Nylon
For stainless mesh, the weekly cleaning procedure is straightforward — remove the infuser from the lid, soak in warm water with 1 teaspoon of citric acid for 15 minutes, brush gently with a soft toothbrush to remove any tea stain, rinse under running water, and air dry. The mesh will return to 95%+ flow on the first soak. For housekeeping before a descaler soak, a baking soda paste (baking soda plus a small amount of water) applied to the mesh for 10 minutes and then scrubbed gently removes any tannin discoloration — the same procedure recommended for the Goodfriends double-layer glass tea maker at the tea house chain.
For nylon mesh, the same procedure will not recover the mesh to baseline. The caprolactam-leached surface is permanently slightly textured after the first 2–3 weeks of hot use, so the mesh continues to bind tannin at an accelerated rate. The practical advice for a nylon-mesh kettle is to schedule a replacement of the mesh every 6 months for a daily-use household, or to switch to a stainless replacement mesh after the original nylon mesh shows visible degradation.
7. When Nylon Still Makes Sense
Despite the longer cleaning interval and the higher end-of-life disposal rate, nylon mesh has its place. Cold-brew tea makers, ambient-temperature tea servers in hotel breakfast buffets, and single-use commercial kettles where the brewer handles the descaling internally are all better served by nylon mesh. The lower unit cost matters when the kettle is part of a hospitality welcome amenity that gets replaced every 12–18 months rather than serviced. For a daily-use home kettle — which is the dominant B2B export segment for the European and North American markets — 304 stainless is the right material.
8. Specifying Filter Mesh in Your Tea Maker Sourcing
For the OEM/ODM buyer, the practical filter-mesh specification for a daily-use export tea maker is 304 stainless steel, 60 mesh count (about 250 micron opening), plain weave, with a stamped frame appropriate for the kettle lid spring-clip geometry. The mesh should be specified as "304 grade per ASTM A240" with a verified mill certificate, and the kettle should carry a food-contact declaration that references the US FDA, EU 1935/2004, and the French DGCCRF Order of January 13, 1976. For the filtered category, this is the same material specification that the major commercial tea chains specify for their brewing equipment.
For buyers specifying a nylon mesh unit for cold-brew or hospitality single-use, the practical spec is PA6 or PA66 with a 40 mesh count (500 micron opening), and the kettle user manual should explicitly call out the 80°C upper temperature limit and the 6-month mesh replacement schedule. Skipping either of these calls in the user manual is a common cause of consumer complaints about taste and clogging in the first quarter of use.
One additional consideration for B2B buyers sourcing tea makers for export: the EU food-contact documentation package. 304 stainless steel mesh with a verified mill certificate to ASTM A240 and an EN 10204 3.1 certification is generally accepted by EU customs without further testing. PA6 or PA66 nylon mesh, on the other hand, requires an EU Regulation 10/2011 overall migration test and a specific migration test for caprolactam (the monomer residual, with a specific migration limit of 15 mg/kg in food simulant). The documentation cost for the nylon mesh declaration is roughly 3–5x higher than the stainless steel mill certificate, and the lead time is 4–6 weeks longer. For a North American buyer, the FDA 21 CFR 177.1500 declaration is needed for both materials, but the FDA does not impose the same monomer-specific testing burden for nylon that the EU does. In practice, the stainless steel mesh is the lower-friction choice for an export product that touches both EU and North American markets.
FAQ
What mesh count is best for a kettle filter?
For loose-leaf tea brewing, 60–80 mesh stainless steel (200–250 micron openings) is the practical sweet spot. Finer mesh (100+) restricts flow too much for full-leaf teas; coarser mesh (40) lets fine particles and small broken leaves pass through.
For loose-leaf tea brewing, 60–80 mesh stainless steel (200–250 micron openings) is the practical sweet spot. Finer mesh (100+) restricts flow too much for full-leaf teas; coarser mesh (40) lets fine particles and small broken leaves pass through.
How often should a kettle filter mesh be cleaned?
Under daily-use hard water (above 200 ppm CaCO3), a nylon mesh needs descaling every 5–7 days; a 304 stainless mesh needs the same treatment every 14–21 days. Soft-water households can extend those intervals by roughly 3x.
Under daily-use hard water (above 200 ppm CaCO3), a nylon mesh needs descaling every 5–7 days; a 304 stainless mesh needs the same treatment every 14–21 days. Soft-water households can extend those intervals by roughly 3x.
Does nylon mesh affect tea taste?
Yes, when hot. Nylon mesh above 80°C starts to leach caprolactam monomer, which contributes a faint plastic off-note. Below 80°C it is generally regarded as safe (FDA 21 CFR 177.1500 and EU 10/2011), but most tea brewing temperatures are above 80°C.
Yes, when hot. Nylon mesh above 80°C starts to leach caprolactam monomer, which contributes a faint plastic off-note. Below 80°C it is generally regarded as safe (FDA 21 CFR 177.1500 and EU 10/2011), but most tea brewing temperatures are above 80°C.
How long does a Stainless Steel Kettle filter last?
A 304 stainless steel filter mesh used in a hard-water household and cleaned weekly with citric acid lasts 4–6 years before the mesh holes begin to widen or the welds at the frame joint start to pit. With soft water and gentler cleaning, the same filter lasts 8–10 years.
A 304 stainless steel filter mesh used in a hard-water household and cleaned weekly with citric acid lasts 4–6 years before the mesh holes begin to widen or the welds at the frame joint start to pit. With soft water and gentler cleaning, the same filter lasts 8–10 years.
Can you put a stainless steel mesh in the dishwasher?
Yes. 304 stainless steel filter mesh is dishwasher safe. Remove the mesh from the kettle lid before running it, and rinse off any loose tea residue first. Avoid dishwasher detergent with chlorine bleach, which can pit the surface over many cycles.
Yes. 304 stainless steel filter mesh is dishwasher safe. Remove the mesh from the kettle lid before running it, and rinse off any loose tea residue first. Avoid dishwasher detergent with chlorine bleach, which can pit the surface over many cycles.
Is 304 stainless steel safe for food contact at boiling temperatures?
Yes. 304 stainless steel is rated for food contact up to 100°C continuous use by the US FDA, EU Regulation 1935/2004, and the French DGCCRF Order of January 13, 1976. Below 100°C, the chromium oxide passive layer is stable and nickel release is below 0.14 mg/kg.
Yes. 304 stainless steel is rated for food contact up to 100°C continuous use by the US FDA, EU Regulation 1935/2004, and the French DGCCRF Order of January 13, 1976. Below 100°C, the chromium oxide passive layer is stable and nickel release is below 0.14 mg/kg.
Does a clogged filter reduce kettle boiling speed?
No. The filter sits in the spout and does not contact the heating element. A clogged filter only affects the pour stream and taste, not the heat-transfer rate. However, a clogged filter is a strong signal that the heating element is also scaling, and the kettle should be descaled.
No. The filter sits in the spout and does not contact the heating element. A clogged filter only affects the pour stream and taste, not the heat-transfer rate. However, a clogged filter is a strong signal that the heating element is also scaling, and the kettle should be descaled.
External References
The 60-day bench test setup above follows the hard-water brewing methodology documented in the InstaCuppa descaling guide for Electric Kettles used in Indian hard-water regions[1]. The mesh cleaning procedures for stainless steel infusers follow the Senbird Tea loose-leaf brewing guide, which documents the 5–10 year service life of a quality stainless mesh infuser under weekly citric acid maintenance[2]. The hard-water kettle selection criteria for limescale-prone households are catalogued in the Mumsnet 2026 hard-water kettle guide, which independently identifies stainless steel interior and concealed element as the two primary material choices for hard-water regions[3]. The nylon off-taste migration at 80°C+ is documented in the food contact compliance notes for US FDA 21 CFR 177.1500 and EU Regulation 10/2011.