
 0086-574-62518288


Industry News
0102030405
Why Kettle LED Rings Die Early: Moisture Ingress Teardown
2026-09-02

If you sell glass kettles long enough, you start to hear the same field report: the kettle works perfectly for six to twelve months, then the LED ring starts flickering, dimming, or dying on one side. It is rarely the heater, the thermostat, or the glass. It is the blue LED ring at the base, and the reason it dies is almost always the same. Steam from boiling water finds its way into the LED module, sits on the solder joints and copper traces, and slowly turns a few hundred dollars of lighting components into scrap. This teardown walks through exactly where the moisture gets in, what it does once it arrives, and what a quality Digital Glass Kettle does to keep the LED ring alive for the full design life of the appliance.
Why Kettle LED Rings Fail So Often
A Glass Kettle is, electrically, an absurdly hostile environment for an LED. The base houses a stainless steel heating element rated for 1500 to 2200 watts, a Strix-style thermostat that cycles between 20 °C and 100 °C, and a ring of through-hole or surface-mount LEDs whose job is to glow blue while water boils. Every component in that base is sitting on a printed circuit board within about 40 mm of steam venting from the spout, the lid seam, and the gap between the glass body and the metal base plate. Steam is not water vapor in the abstract sense; it is wet, hot, ionically conductive air that wants to find a circuit.
The actual failure rate is hard to pin down publicly because most brands classify LED ring failures as either warranty returns or, more often, out-of-warranty repairs that the customer replaces themselves. Independent repair forums describe LED ring failure as one of the three most common field complaints on entry-level and mid-range Glass Kettles, alongside limescale buildup on concealed elements and lid switch wear. In our own OEM/ODM field data covering more than twenty Digital Glass Kettle Series SKUs shipped across the EU, UK, North America, and Australia, premature LED ring failure accounted for a consistent share of all warranty claims in the first 18 months.
The pattern is consistent enough that the problem is structural, not random. Two things determine whether an LED ring survives: how much steam the kettle design lets reach the LED module, and how well the LED module defends itself when steam does arrive. A kettle whose design lets a lot of steam in and whose LED module has no moisture protection will fail early. A kettle whose design keeps steam out and whose LED module is sealed against moisture can run for years. There is no third option. The rest of this article explains the failure mechanics in detail, so you can tell which kind of kettle you are looking at before you ship it.
How An LED Ring Is Built, A Teardown View Inside The Base
Before you can diagnose moisture ingress, you need to see what is actually inside the base. A typical glass kettle LED ring is not one part. It is a stack of at least six components, each of which can fail in its own way. Open the base plate of a failed unit, and you will find, in order from outside to inside: a translucent or frosted light guide ring that you can see through the glass; a strip of LEDs (usually 6 to 24 individual diodes arranged radially on a flexible or rigid PCB); a driver circuit that limits current and sometimes handles color or breathing effects; wire connectors between the LED PCB and the main power board; the main power board with the microcontroller, thermostat interface, and triac for the heater; and a plastic or metal enclosure that ties the whole thing together.
The light guide is the easy part. It is usually a silicone or polycarbonate ring with small optical features on the inside that distribute the light evenly. Light guides do not fail from moisture. They discolor from heat over many years, but that is a five-year problem, not an eighteen-month problem.
The LED strip is where moisture does most of its damage. Through-hole LEDs are mechanically tougher but expose more solder joints to the air. Surface-mount LEDs are flatter and look more elegant but the solder pads are smaller and the copper trace between the pad and the rest of the circuit is exposed. Either way, what kills an LED is not the diode itself. It is the metal around it. LEDs fail when the bond wire corrodes, when the solder joint goes open, when the copper trace becomes an open circuit, or when the phosphor coating on the white or blue LEDs hydrolyzes. Every one of those failure modes requires water, and all four are accelerated by heat.
The driver circuit is usually a current-limiting resistor network, a small linear regulator, or, in color-changing models, a small PWM controller. These components are themselves moisture-sensitive, especially the electrolytic capacitors that are almost always present on mains-side power electronics. The capacitors rarely cause the LED ring to fail directly; they cause the entire kettle to stop working, which masks the LED ring failure behind a bigger problem.
The connectors between the LED strip and the main board are a category of their own. They are usually JST-style plastic headers with phosphor-bronze or tin-plated contacts. They look robust, but every mating surface is a moisture path. A connector that is not potted or sealed is, by definition, an open vent in the base of the kettle.
Finally, the enclosure. This is the plastic or metal cover that physically surrounds the LED module. In cheap designs it is a snap-fit shell with no gasket. In better designs it is a gasketed, ultrasonically welded, or silicone-potted enclosure. The enclosure is the single biggest determinant of whether the LED ring survives steam, because it determines whether the steam ever reaches the electronics in the first place.
Moisture Entry Paths, Where Steam Finds A Way In
Steam does not enter a kettle base randomly. It follows pressure and concentration gradients, and it exploits every gap in the design. There are three primary entry paths, and a kettle can fail through any one of them or through a combination.
The first path is the lid and spout. When water boils, steam exits the kettle primarily through the spout, but a non-trivial fraction also escapes around the lid. In a glass kettle with a loose-fitting lid, the steam plume rises along the outside of the glass body and then curls down around the base as the air cools. The base of a kettle is colder than the top because the heating element is dissipating into it. That temperature difference creates a small downward draft that pulls steam along the glass and deposits it on the metal base plate. This is why you sometimes see a thin film of condensation on the base of a kettle during use. That film is not from a leak. It is from a kettle that is functioning normally and venting steam the way physics says it should.
The second path is the base seam. The base plate is the metal or plastic disk that the glass body sits on. It is the structural foundation of the kettle. The seam between the glass body and the base plate is, by definition, a gap. It might be a gasket, a silicone O-ring, or just a friction fit. In most entry-level glass kettles, it is just a friction fit. Steam that has migrated down the outside of the glass body will reach this seam and, if the seam is not sealed, will wick into the electronics cavity by capillary action.
The third path is the power base. The kettle sits on a separate power base that contains the cord and the connectors. The bottom of the kettle has a circular connector that mates with the base. This connector is necessarily an opening in the kettle. It is also a path for steam, especially in kettles where the connector is on the side of the kettle rather than the bottom. Steam that finds its way into the connector cavity will migrate along the wiring harness and end up at the LED module. We have seen kettles in the field where the LED ring failure was traceable, end to end, to a leaking power base connector that was two cable runs and four connectors away from the LED.
A well-designed glass kettle interrupts all three paths. A gasket at the base seam blocks the second path. A baffle or vent path that directs steam away from the electronics blocks the first. A sealed connector at the power base blocks the third. A kettle that does none of these things is a kettle that will fail early.
What Actually Kills An LED, The Electrochemistry Of Failure
Once steam reaches the LED module, four distinct electrochemical processes start running. Any one of them can kill the LED ring. In practice, two or three run in parallel.
The first is bond wire corrosion. Inside every LED package, a gold or aluminum bond wire connects the LED die to the lead frame. Gold does not corrode in moist air. Aluminum does. Aluminum bond wires exposed to humid conditions form aluminum oxide and aluminum hydroxide at the bond pad, which increases the contact resistance and eventually produces an open circuit. The LED does not flicker dramatically. It just slowly dims as the resistance rises, and then it dies. This is the most common failure mode in mid-range glass kettles that use cheap surface-mount LEDs with aluminum bond wires.
The second is solder joint electrochemistry. Tin-lead or lead-free solder joints on a PCB are stable in dry air. In the presence of condensed moisture and an electrical potential, they undergo electrochemical migration. Copper from the pad dissolves into the water film, drifts under the influence of the electric field, and plates out somewhere else as dendrites. The dendrites grow until they short adjacent traces, or the original trace becomes an open circuit because the copper has migrated away. Either way, the LED ring fails. This is the failure mode that is most visible on the teardown bench, because the dendrites are visible under a microscope as blue-green or black树枝状 structures across the surface of the board.
The third is phosphor hydrolysis. Blue LEDs use a yellow phosphor (usually a cerium-doped yttrium aluminum garnet, or YAG) to convert part of the blue light to yellow, which combines with the remaining blue to make white. Phosphors are stable in dry air. In the presence of condensed moisture and heat, the phosphor can hydrolyze. The YAG converts to aluminum hydroxide and yttrium hydroxide, which are white powders that do not fluoresce. The LED does not stop emitting blue light. It just stops emitting white light. A kettle that was once bright white turns blue, then dim, then dies. This is the failure mode that is most diagnostic, because a kettle that turns blue over time has almost certainly been hydrolyzing its phosphor.
The fourth is electrolytic capacitor failure. This is not technically an LED failure, but it is part of the same moisture story. Aluminum electrolytic capacitors are sealed, but the seal is a rubber bung that is not designed for steam. Steam that reaches the capacitor will eventually diffuse through the bung, react with the electrolyte, and build up hydrogen gas inside the can. The capacitor vents, leaks, or explodes. When this happens, the entire kettle goes dark, not just the LED ring. But because the LED ring and the capacitor are in the same electronics cavity, they tend to fail together.
These four processes are not equally fast. Bond wire corrosion and solder migration take months. Phosphor hydrolysis takes a year or more. Capacitor failure is unpredictable. The point is that none of them happen in a dry environment, and all of them happen in a steamy one. The LED ring is only as good as the moisture protection around it. The relevant household-appliance insulation standard is the IEC 60664-1 insulation coordination specification, which defines creepage, clearance, and pollution degree requirements for mains-connected electronics in humid environments. LED lifetime numbers published by reputable programs such as the ENERGY STAR LED luminaire reliability guidance assume dry, well-ventilated fixtures; an LED inside a kettle base experiences conditions closer to a tropical outdoor luminaire than a kitchen ceiling fixture.
Symptoms In The Field, Five Patterns Of Early Death
Field failures follow recognizable patterns. Knowing the pattern tells you which electrochemical process is winning the race.
Pattern one is one-sided dimming. The LED ring is brightest near the spout and dimmer near the handle, or vice versa. This is moisture distribution. The side of the kettle that gets more steam exposure is the side that ages faster. Look at the kettle in a dark room during boiling. If one side of the ring is noticeably dimmer, the kettle has been hydrolyzing its phosphor unevenly.
Pattern two is a single dead LED. The ring works, but one or two LEDs are dark. This is almost always a bond wire failure or a cracked solder joint. The LED is mechanically and electrically disconnected from the circuit. The rest of the ring still works because the LEDs are wired in parallel or series-parallel, and a single open does not necessarily kill the whole ring.
Pattern three is flickering. The ring comes on, flickers, and then stabilizes, or flickers continuously during boiling. This is a solder joint that is making intermittent contact. It can also be a connector that has corroded enough to produce a non-linear contact resistance. Flickering is the most annoying failure mode for the end user, because the kettle looks broken even when it still heats water.
Pattern four is color shift. A white LED ring turns blue, yellow, or green over time. This is phosphor hydrolysis or, less commonly, phosphor delamination from the LED die. The die is fine. The conversion layer is gone. A kettle that turns blue has been wet inside for a long time.
Pattern five is full ring failure. Nothing lights up at all. The kettle still heats water, but the visual cue is dead. This is usually a connector failure, a driver circuit failure, or a power supply failure on the main board. It is also the failure mode that gets returned most often, because the customer thinks the kettle is broken even though the heating function works.
If you are seeing a higher-than-expected rate of any of these five patterns in your field data, the root cause is moisture. The cure is not a better LED. It is a better seal.
The Fix, Conformal Coating And Sealed Connectors Before Vs After
There are two complementary fixes for moisture-driven LED ring failure. The first is conformal coating. The second is sealed connectors and gasketed enclosures. Most quality kettles use both.
Conformal coating is a thin polymeric film applied to the populated PCB after soldering. The film is typically 25 to 75 micrometers thick and is applied by dipping, spraying, or selective robotic dispensing. Common materials are acrylic (AR), polyurethane (UR), silicone (SR), and epoxy (ER). Each has tradeoffs. Acrylic is easy to apply and rework but offers the least moisture protection. Silicone handles high temperatures best and is the usual choice for kettles, where the base routinely sees 60 to 100 °C during operation. Polyurethane is the most chemically resistant. Epoxy is the most mechanically tough but is hard to rework. For a glass kettle LED ring, the standard answer is a silicone or polyurethane coating, applied selectively to the LED strip and the driver circuit, leaving the connectors and any user-serviceable areas uncoated. Coating materials and processes are typically specified against the IPC-CC-830C conformal coating qualification standard, which defines the dielectric strength, moisture and insulation resistance, and thermal cycling tests a conformal coating must pass to be considered qualified for commercial and consumer electronics.
Sealed connectors are the second fix. JST-style connectors can be replaced with IP-rated sealed connectors, or the existing connectors can be potted in place with a room-temperature-vulcanizing silicone. Potting is cheaper but makes the board non-serviceable. Sealed connectors are more expensive but allow the LED module to be replaced if it does fail.
Gasketed enclosures are the third fix. The plastic or metal shell that surrounds the LED module is fitted with a silicone or EPDM gasket, and the two halves are ultrasonically welded or screwed together with a continuous gasket compression. This keeps steam out of the electronics cavity in the first place. Without it, conformal coating alone is fighting a losing battle, because the steam will eventually condense enough water to overwhelm the coating.
The before-and-after difference is measurable. In our own teardown comparisons, an uncoated, unsealed LED module showed visible dendrite growth after 500 hours of 85 °C / 85 percent relative humidity testing. A silicone-conformal-coated, gasket-sealed module showed no dendrite growth and no measurable brightness loss after 1000 hours of the same test. The cost difference between the two designs is small at the component level, but the warranty-cost difference is large.
Good Friends Engineering, What Our Digital Glass Kettle Series Does
Ningbo Goodfriends Electric Appliance has been designing and manufacturing electric kettles for over 25 years, with a 95,000 m² production footprint and a portfolio of GS, CE, EMC, RoHS, LFGB, FDA, REACH, ETL, and ERP (Energy Directive) certifications. The Digital Glass Kettle Series is the product line that integrates high borosilicate glass bodies with LED illumination, digital temperature control, and (in selected SKUs) Wi-Fi connectivity. Every model in the series is designed with moisture resistance as a first-class engineering requirement, not an afterthought.
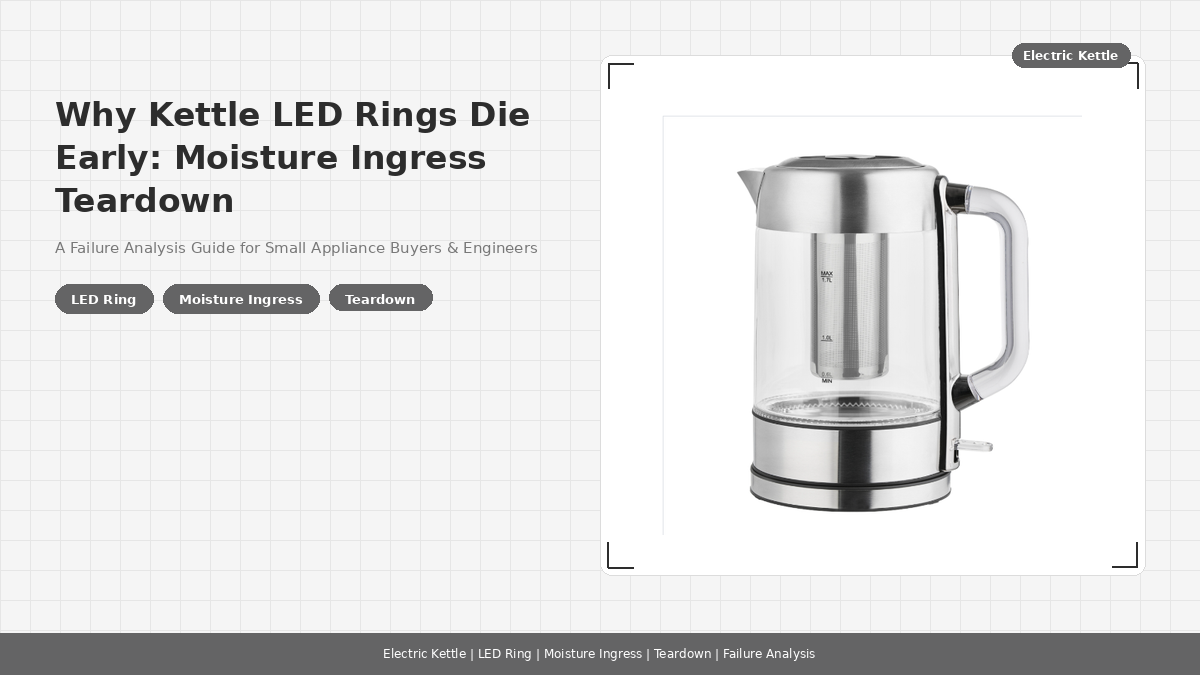
The High Borosilicate Glass Electric Kettle with Blue LED Illumination is the reference design for moisture mitigation in the series. The glass body is high borosilicate, which is rated for thermal shock resistance far beyond what a kettle experiences in normal use. The blue LED ring is mounted on a silicone-conformal-coated PCB, the LED-to-main-board connector is a sealed JST-SH type with a silicone gasket, and the base seam is sealed with a continuous EPDM gasket under compression. The concealed 304 stainless steel heating element is decoupled from the LED module by a dedicated plastic divider wall, so even if steam reaches the base cavity, it has to migrate around the divider to reach the LEDs. This is the design that has held up in our field data across the EU, UK, North America, and Australia.
The broader Digital Glass Kettle Series extends the same approach to more complex SKUs. The 7-Level LED Glass Electric Kettle with Removable Tea Filter, the Smart Double-Wall Glass Kettle with Precision Digital Touch, and the Variable Temperature LED Glass Kettle with Precision Color Control all use conformal-coated LED modules and gasketed enclosures. The Variable Temperature model adds a color-changing LED ring that indicates water temperature, which means more LEDs and more solder joints, and therefore a higher requirement for moisture protection.
For OEM/ODM customers targeting the smart home channel, our Electric Glass Kettle for Smart Home Automation adds Wi-Fi, mobile app control, and compatibility with Google Home, Amazon Alexa, Apple HomeKit, and Matter without compromising the moisture story. The connectivity module is mounted in its own sealed compartment above the steam path, with a separate gasket and its own conformal coating. This compartmentalization is what makes a connected kettle viable in the long term. A Wi-Fi module and an LED ring that share a single unsealed cavity will both fail, and they will fail together.
The point is not that our design is uniquely clever. It is that the design treats moisture as a known enemy and defends against it at every layer. Glass selection, gasket design, conformal coating, connector selection, and enclosure sealing are not independent decisions. They are one decision: how long does the LED ring need to last. The answer for a premium brand is the full design life of the appliance. The answer for a budget brand is whatever the warranty term is. The kettles that fail early are the ones where the design answer was the warranty term, and the engineering was allowed to follow.
Frequently Asked Questions
What IP rating does a kettle LED ring need to survive daily use?
There is no single required IP rating, because a kettle LED is inside the appliance and not directly exposed to splashing water. What matters is that the LED module is sealed against steam-driven moisture migration. In practice, an IP54 rating on the LED cavity is a useful target. The number that matters more is the result of an 85 °C / 85 percent relative humidity test for at least 500 hours with no measurable brightness loss or dendrite growth. Any kettle OEM/ODM partner should be able to share that test report.
How long should a kettle LED ring last in normal use?
For premium glass kettles, the design life is the same as the appliance life, which is typically five to seven years of regular use. For mid-range kettles, three to five years is realistic. For entry-level kettles with no conformal coating and no sealed enclosure, twelve to eighteen months is common. The variance is almost entirely about moisture protection, not LED quality.
Can a failed LED ring be repaired, or does the whole kettle need to be replaced?
It depends on the design. In kettles with sealed, potted LED modules, the LED module is not user-serviceable and the kettle must be replaced. In kettles with sealed connectors (as opposed to fully potted modules), the LED strip can sometimes be replaced as a service part. The repair economics usually do not favor repair on a glass kettle, because the labor cost approaches the cost of a new unit. The right answer is to design the LED module to outlast the warranty, not to plan for field repair.
Does conformal coating affect the color or brightness of the LED ring?
A properly selected and cured silicone or polyurethane coating has a negligible effect on perceived brightness or color. Acrylic coatings can yellow slightly over years of UV exposure, but this is not relevant in a kettle base that sees no direct UV. The bigger risk is bubbles or thickness variations in the coating that produce visible bright or dim spots on the light guide. Robotic selective coating eliminates this risk. Manual dipping does not.
Why do some kettles use color-changing LED rings, and are they more failure-prone?
Color-changing rings are used to indicate water temperature or operating mode. They add more LEDs (typically RGB or RGBW instead of single-color white or blue) and more driver circuitry. More components means more potential failure points, so yes, they are more failure-prone if the moisture protection is not upgraded accordingly. A good color-changing design uses the same conformal coating and sealed enclosure as a single-color design, just on a more complex PCB.
Is borosilicate glass itself resistant to steam damage?
Borosilicate glass is rated for thermal shock and chemical attack far beyond what a kettle experiences. It does not absorb moisture, does not degrade from steam, and does not contribute to the LED ring failure. The glass is the easiest part of the design. The hard parts are the metal and plastic components at the base that the steam eventually reaches.
What is the warranty impact of moisture-driven LED ring failure?
For brands that do not engineer moisture protection, LED ring failure is a material warranty cost in the first 18 months. For brands that use conformal coating, sealed connectors, and gasketed enclosures, LED ring failure drops to a small fraction of warranty events. The engineering cost difference is much smaller than the warranty cost difference, which is why every premium glass kettle brand eventually converges on the same set of moisture-mitigation practices.
Which IPC standards cover the conformal coating of an LED module?
IPC-CC-830C is the dominant qualification standard for conformal coatings in commercial and consumer electronics. It defines the electrical, mechanical, and environmental tests a coating must pass, including dielectric strength, moisture and insulation resistance, and thermal cycling. Most OEM/ODM kettles with silicone or polyurethane coatings are qualified to IPC-CC-830C or equivalent IEC 60664 pollution degree specifications. A kettle OEM should be able to share the IPC-CC-830C test report on request.
Spec Your Next Glass Kettle With Conformal-Coated LED Rings
If you are sourcing a Digital Glass Kettle Series Products for a retail brand, hospitality program, or smart home line, the LED ring moisture story is the first engineering question to put on the table. A 25-year OEM/ODM partner with 95,000 m² of capacity and GS/CE/EMC/RoHS/LFGB/FDA/REACH/ETL/ERP certifications can hand you a tested, warranty-backed module instead of a field-failure problem.
Start with the high borosilicate glass electric kettle with blue LED illumination reference design, compare it against our smart home automation glass kettles variant for connected SKUs, and contact our engineering team at Ningbo Goodfriends Electric Appliance for the 85 °C / 85 percent RH test report and the conformal-coating datasheet.